Cleaning Chemicals for Foundries & Die Casting Plants
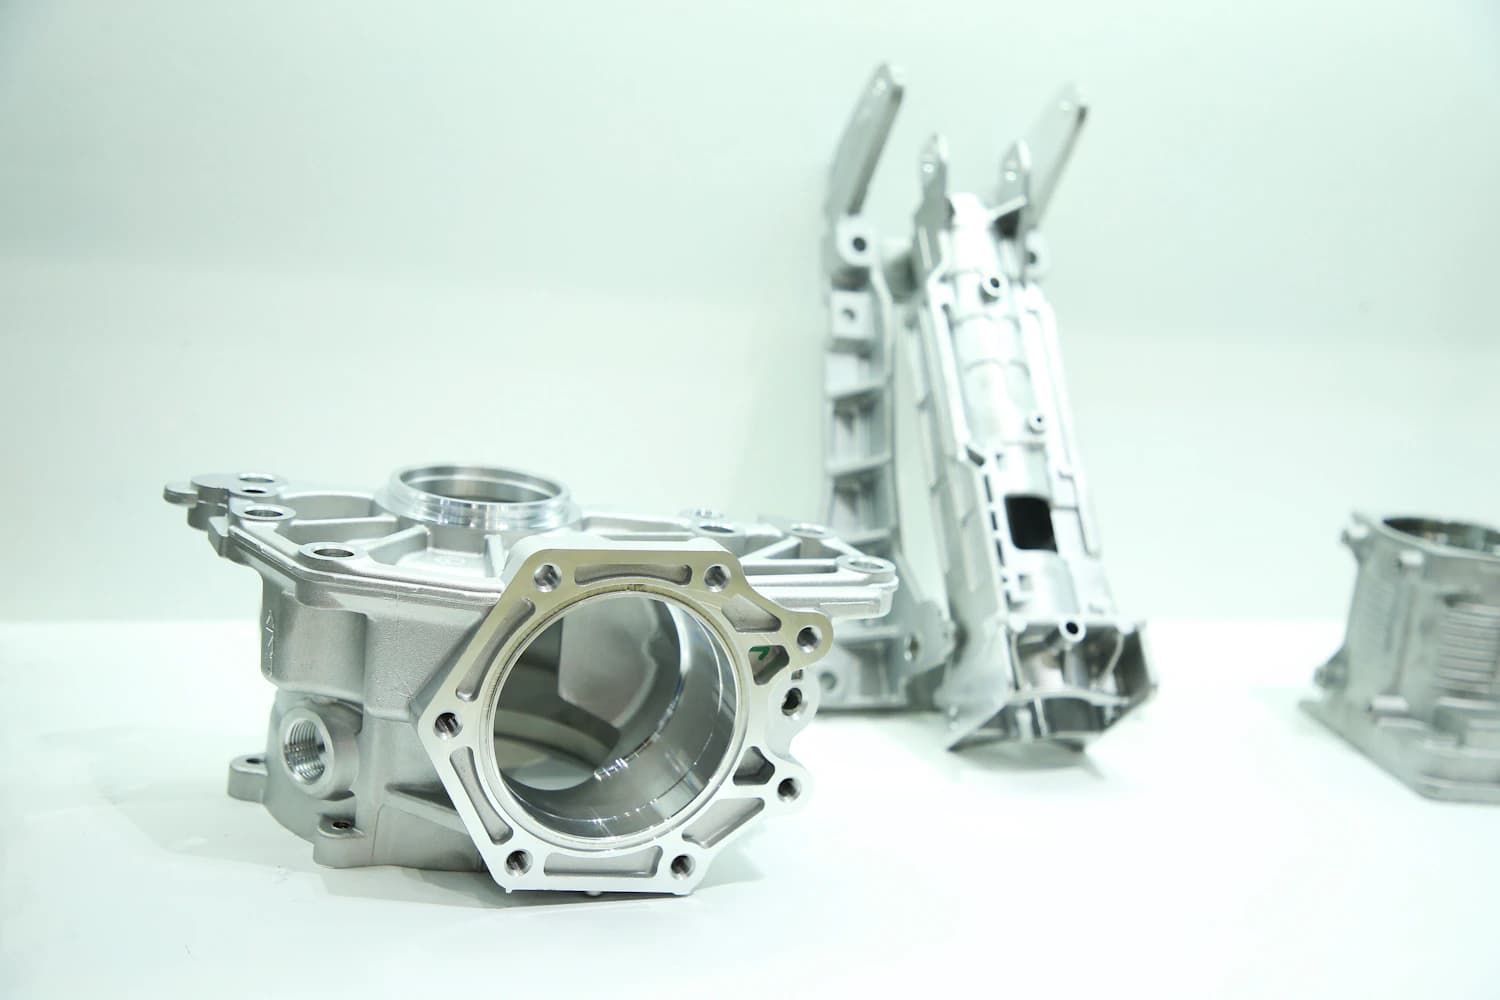
Die casting brings a specific and expensive failure mode: parts leave the wash looking fine and arrive at the customer covered in white bloom. The cause is almost always chemical — an alkaline cleaner etching the alloy — compounded by parts packed before they were genuinely dry.
The short answer
Aluminium die castings must be cleaned with neutral-pH chemistry at 55–65 °C. Alkaline cleaners above pH 10 etch ADC10 and ADC12, leaving a reactive surface that blooms into white rust within days. Switching to a neutral cleaner with a controlled dry has cut white-rust rejection from 3.2% to 0.4% in Power Clean field data.
- Cleaner pH
- Neutral, 7–9
- Concentration
- 2–4%
- Wash temperature
- 55–65 °C
- Critical stage
- Complete drying before packing
- Measured result
- 3.2% → 0.4% white-rust rejection
The Foundry & Die Casting Failure Modes
These are the problems we are called in for most often in this sector — and what causes each one.
Alkalinity etches the alloy
ADC10 and ADC12 are alkali-sensitive. Above about pH 10 the cleaner attacks the surface, dulling it and exposing fresh reactive metal — the precondition for white rust.
Die release agent and lubricant
Release agents are formulated to be persistent. They need adequate surfactancy and dwell, which a neutral cleaner supplies through chemistry rather than caustic strength.
Water trapped in blind features
Castings are full of blind holes and pockets. Rinse water left in them and sealed into packaging creates a humid microclimate that grows white rust in days.
Porosity and machining fines
Cast porosity holds fluid and fines that bleed out later. Adequate rinse dwell and drying time are not optional on porous castings.
What We Recommend
Where It Is Used
- Aluminium die casting cleaning
- ADC10 and ADC12 component cleaning
- Die release agent removal
- Aluminium cleaning and brightening
- White rust prevention
- Machining fines removal
- Bin and tray washing
Foundry & Die Casting Cleaning — FAQ
Why do aluminium castings develop white rust after washing?
Two causes, usually together. An alkaline cleaner above pH 10 etches the alloy and leaves a reactive surface; and rinse water trapped in blind holes creates a sealed humid pocket in packaging. Neutral-pH chemistry plus complete drying eliminates both.
What pH cleaner should be used on ADC12?
Neutral, between pH 7 and 9. ADC12 is an aluminium-silicon-copper alloy that is attacked by alkalinity. A neutral-pH cleaner such as Power Clean NF-14 removes oil and release agent without etching the surface.
How much can white rust rejection actually be reduced?
Power Clean field data on aluminium die-cast housings records white-rust rejection dropping from 3.2% to 0.4% after switching from an alkaline cleaner to neutral-pH NF-14 with a controlled drying stage.
Run a Trial on Your Foundry & Die Casting Line
Send a sample part with your soil and wash equipment details. The lab matches a formulation and returns a dosing and trial plan before anything ships in volume.
Prefer to talk? Call +91-9731727868WhatsApp us